Honed Tube vs SRB Tube: Which Bore Finish Do You Need?
Honing and skived & roller burnishing both finish a cylinder bore — but the surface, the speed and the best use are different. Here is how to choose.
Two ways to finish a bore
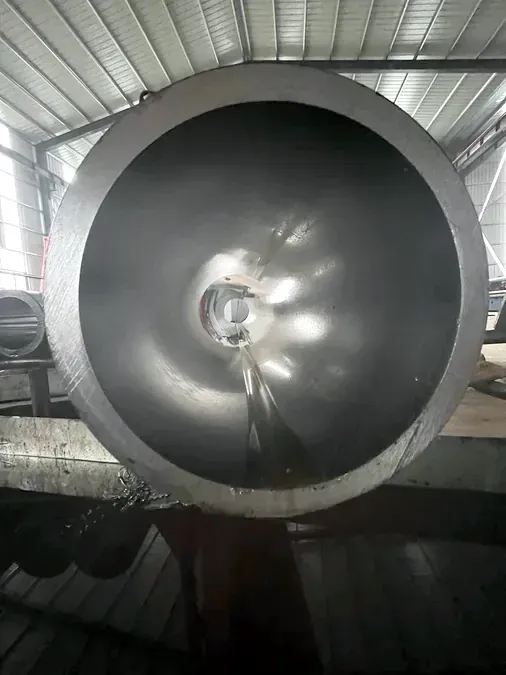
A cylinder barrel starts as a cold-drawn tube. Honing grinds the bore with abrasive stones to size and finish. Skiving and roller burnishing (SRB) cuts the bore with a skiving tool, then rolls it smooth with hardened rollers.
Surface and tolerance
A honed bore is typically Ra 0.2–0.4 um with an ISO H8/H9 tolerance. An SRB bore reaches Ra 0.2 um with the same H8/H9 tolerance, and its fine cross-hatch holds oil on the sealing surface. Both bores arrive ready to use — no further boring.
Which one to choose
Choose honing when the bore needs heavier stock removal or a specific cross-hatch. Choose SRB for high-volume barrels where a smoother bore and a shorter cycle help. Tell us the cylinder duty, the seal type and the operating pressure, and we confirm the finish in quotation.
Standards and materials
Both processes use the same starting tube: E355 (ST52), CK45 and SAE 1026 to EN 10305-1 and EN 10305-4. Cut to length, chamfered, bore protected with anti-rust oil and end caps.